Infrastructure built for sterile production
A greenfield plant has the ability to adapt to the improving manufacturing practices of the industry. With the revised Schedule M guidelines pushing for higher standards of manufacturing, the Qalys plant is designed in compliance with PIC/S standards.
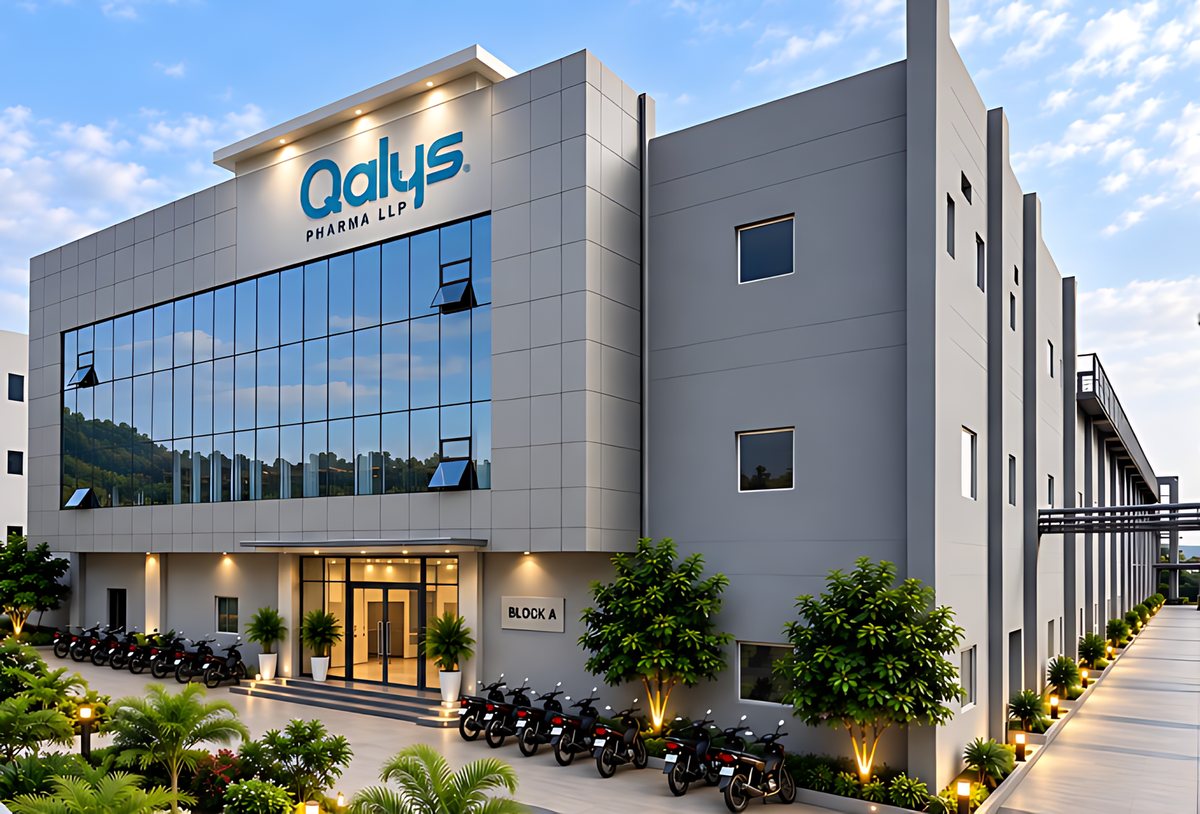
What’s inside the plant
Each part of the facility exists to protect one thing: the sterility and consistency of the product that reaches the patient.
ISBM bottle technology
Qalys specialises in Injection Stretch Blow Moulding, which forms IV bottles in an automated, controlled process for consistent, transparent containers.
Cleanrooms with HEPA filtration
Modern HVAC with complete HEPA filtration protects every batch from cross-contamination during preparation and filling.
Automated high-speed filling
Automated filling lines built for optimised output dose and seal containers with reduced manual handling.
Efficient water system
A water system built around efficiency. We recycle up to 96% of the water used in the process, minimising waste and reducing redundant costs, and a dedicated VCD system brings operational advantages and higher water output.
Quality control laboratory
Raw material analysis, HPLC testing where applicable and stability studies under applicable climatic conditions.
Storage & supply
Large production capacity combined with robust storage facilities keeps supply reliable.
The Qalys Markers
Using state-of-the-art machinery, Qalys specialises in the ISBM space and can deliver up to 8 million bottles a month, all sterilised at 121 °C, to meet the standards expected by our partners at home and abroad.
Think Quality, Think Qalys
Manufacturing pharmaceutical products needs attention to detail at every step. From selecting raw materials to the final packing of products, quality remains an important part of how we work.
Our manufacturing approach focuses on:
- Following established pharmaceutical manufacturing practices.
- Reduced human intervention to minimise contamination.
- Checking product quality at every stage of manufacturing.
- Following validated sterilisation procedures, wherever applicable.
- Carrying out necessary quality checks before product release.
- Maintaining proper manufacturing and quality records.
- Working in accordance with applicable regulatory requirements.
IV fluid packaging, designed for safe and convenient administration
Packaging is an important part of IV fluid manufacturing. It must protect the product, maintain its quality and make handling and administration convenient for healthcare professionals. We give importance to packaging design, container strength, transparency, closure integrity and suitability for the intended pharmaceutical formulation.
Sterilisation
Containers suited to validated terminal sterilisation processes, including 121 °C cycles, wherever applicable.
Collapsible design
Containers designed to collapse during administration, depending on the packaging system.
Adequate headspace
Enough space in the container to add compatible medicines when required.
Product visibility
Transparent containers that make it easy to check the solution visually.
Secure closure
Proper closure systems that help protect product integrity.
Drug compatibility
Packaging suitability is evaluated for specific formulations, including selected oncology medicines.
Plan production with Qalys
Discuss volumes, timelines and documentation for contract manufacturing or supply partnerships.